
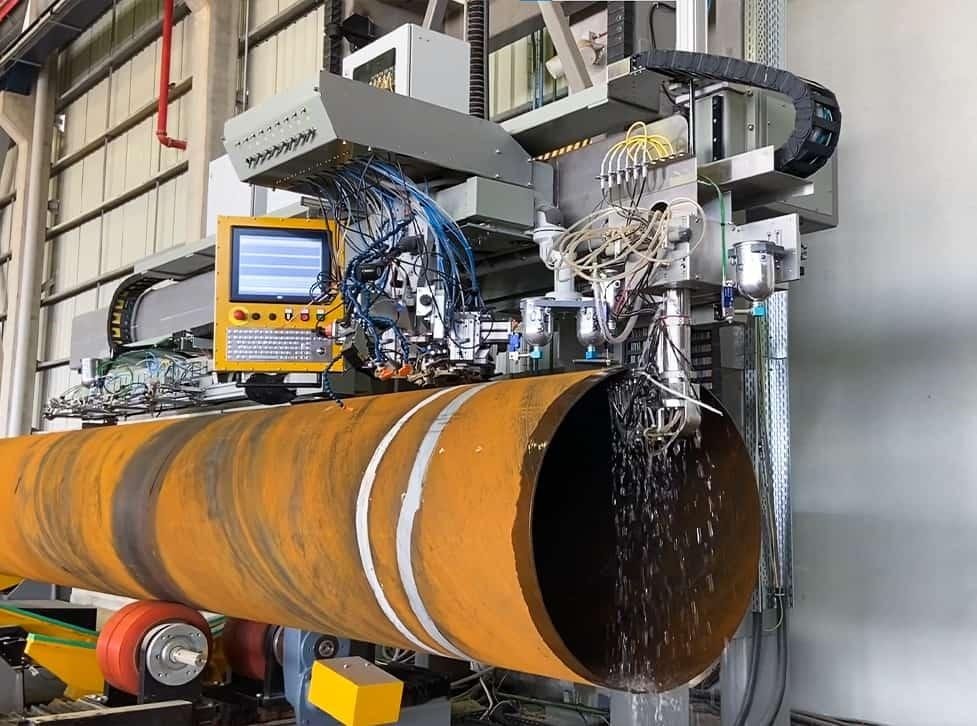
1. Introduction: Why Are Hydrostatic Testing and NDT Important for Steel Pipes?
Steel pipes used in oil and gas, petrochemical processing, power generation, water transportation and industrial construction must meet specific quality and safety requirements before delivery.
Manufacturing defects, welding discontinuities, cracks, wall thickness variations and leakage can affect the mechanical performance and service reliability of steel pipes.
To verify product quality, manufacturers use different inspection and testing methods throughout production.
Two important categories are hydrostatic pressure testing and nondestructive testing (NDT).
Although both are used to evaluate steel pipe quality, they serve different purposes.
Hydrostatic testing uses pressurized water to verify the pressure integrity of a pipe under specified test conditions. NDT methods use physical techniques such as ultrasound, electromagnetic induction, magnetic fields and liquid penetrants to identify particular types of material discontinuities without damaging the product.
The main difference is that hydrostatic testing evaluates pressure integrity, while conventional flaw-detection NDT methods evaluate specific defects or discontinuities.
Neither method provides a complete assessment of every possible pipe defect. For this reason, steel pipe manufacturers often combine several inspection methods to meet product standards and purchaser requirements.
This guide explains the differences between hydrostatic testing and NDT, their working principles, common inspection methods, applicable standards and practical applications.
2. What Is Hydrostatic Testing of Steel Pipes?
Hydrostatic testing is a pressure test that uses water or another suitable liquid as the test medium.
During the test, the pipe is filled with liquid, air is removed as required by the procedure, and internal pressure is increased to the specified test level.
The pressure is maintained for the required period while the pipe is monitored for leakage and other signs of pressure-boundary failure.
The purpose is to verify that the tested pipe can withstand the specified test pressure without unacceptable leakage or failure.
2.1 How Does a Hydrostatic Test Work?
A typical steel pipe hydrostatic testing process includes the following steps:
Step 1: Initial Inspection
The pipe is checked for visible damage, dimensional irregularities and conditions that could affect safe testing.
Step 2: Pipe Filling
The pipe is filled with water or another specified liquid. Suitable venting arrangements are used to remove trapped air.
Step 3: End Sealing
Appropriate test heads or end closures are installed to prevent leakage from the pipe ends.
Step 4: Pressure Application
A hydraulic pump gradually increases the internal pressure to the specified test pressure.
Step 5: Pressure Holding
The required pressure is maintained for the specified duration. Pressure readings and relevant test conditions are recorded.
Step 6: Leakage Inspection
The pipe is examined for visible leakage, pressure instability and other unacceptable indications.
Step 7: Depressurization and Documentation
Pressure is safely released, the pipe is drained where necessary, and the test results are recorded.
The test procedure must follow the applicable product standard, approved testing procedure and contractual requirements.
2.2 What Does Hydrostatic Testing Detect?
Hydrostatic testing can help identify:
- Through-wall leakage.
- Pressure-boundary weaknesses.
- Defects that become leakage paths under the applied test conditions.
- Certain manufacturing or welding defects that compromise pressure integrity.
- Inadequate pressure containment under the specified test conditions.
However, hydrostatic testing does not reliably identify every internal crack, inclusion, lamination or localized discontinuity.
A pipe can pass a hydrostatic test while still containing defects that do not cause leakage at the specified test pressure and duration.
Therefore, passing a hydrostatic test does not mean that the pipe is free from all manufacturing defects.
2.3 Advantages of Hydrostatic Testing
Hydrostatic testing offers several advantages:
- Directly evaluates pressure integrity.
- Can identify leakage through the pipe wall.
- Provides a documented pressure test result.
- Is widely incorporated into steel pipe product specifications.
- Can be performed on individual pipe lengths using automated testing equipment.
2.4 Limitations of Hydrostatic Testing
Despite its importance, hydrostatic testing has limitations:
- It does not provide a detailed map of internal material defects.
- Small or non-through-wall discontinuities may remain undetected.
- It does not directly measure remaining wall thickness.
- It cannot independently establish the full mechanical properties of the material.
- It requires appropriate end closures, pressure equipment and safety controls.
- Water residues may require drainage and drying, particularly for corrosion-sensitive applications.
Hydrostatic testing should therefore be considered one part of a complete inspection program rather than a replacement for all other inspection methods.
3. What Is Nondestructive Testing (NDT) of Steel Pipes?
Nondestructive testing refers to inspection techniques used to evaluate material condition without destroying or permanently damaging the tested component.
In steel pipe manufacturing, NDT is used to detect different types of discontinuities in the pipe body, weld seam and other critical areas.
Common methods include:
- Ultrasonic Testing (UT).
- Eddy Current Testing (ET).
- Magnetic Particle Testing (MT).
- Liquid Penetrant Testing (PT).
- Radiographic Testing (RT).
- Magnetic Flux Leakage (MFL).
- Electromagnetic Inspection (EMI).
Each technique operates on a different physical principle and has its own detection capabilities and limitations.
3.1 Ultrasonic Testing (UT)
Ultrasonic testing uses high-frequency sound waves to examine the material.
A transducer sends ultrasonic waves into the pipe. Changes in the reflected signals can indicate material boundaries, wall thickness variations or discontinuities.
Depending on the technique and inspection procedure, UT can detect:
- Internal cracks.
- Laminations.
- Inclusions.
- Wall thickness reduction.
- Weld discontinuities.
- Certain surface-connected defects.
UT is widely used for seamless steel pipes and welded pipe inspection.
Automated ultrasonic testing systems can inspect large numbers of pipes during manufacturing.
Its performance depends on probe frequency, calibration, surface condition, coupling, pipe geometry and the orientation of the discontinuity.
3.2 Eddy Current Testing (ECT)
Eddy current testing uses electromagnetic induction to detect discontinuities in electrically conductive materials.
An alternating current in the inspection coil produces a changing magnetic field, which induces eddy currents in the steel pipe.
Defects and changes in material conditions affect the electromagnetic response detected by the equipment.
ECT is particularly useful for identifying certain surface and near-surface discontinuities in tubular products.
Applications include:
- Seamless steel tubes.
- Welded steel tubes.
- Heat exchanger tubes.
- Thin-wall tubular products.
ECT is sensitive to material properties, probe configuration, frequency, geometry and test conditions.
It is not a universal replacement for ultrasonic inspection, particularly when deeper internal defects must be evaluated.
3.3 Magnetic Particle Testing (MT)
Magnetic particle testing is used to identify surface and near-surface discontinuities in ferromagnetic materials.
The steel component is magnetized, and magnetic particles are applied to the inspection area.
Discontinuities that disturb the magnetic field can produce leakage fields that attract the particles.
Common applications include detecting:
- Surface cracks.
- Weld toe cracks.
- Grinding cracks.
- Near-surface discontinuities.
- Certain manufacturing defects.
MT is suitable for carbon steel and other ferromagnetic materials but is generally not suitable for non-ferromagnetic stainless steel grades.
3.4 Liquid Penetrant Testing (PT)
Liquid penetrant testing identifies surface-breaking discontinuities.
A penetrant liquid is applied to the cleaned surface and allowed to enter surface openings through capillary action.
After excess penetrant is removed, a developer is applied to draw penetrant back out of the discontinuities, making indications visible.
PT can identify:
- Surface cracks.
- Porosity open to the surface.
- Surface-breaking seams.
- Other open-to-surface discontinuities.
It cannot reliably detect defects located entirely beneath the material surface.
PT can be used on both ferromagnetic and non-ferromagnetic materials, provided the surface condition and inspection procedure are suitable.
3.5 Radiographic Testing (RT)
Radiographic testing uses X-rays or gamma rays to produce an image of the internal structure of a material.
Differences in radiation absorption can reveal certain internal discontinuities.
RT is commonly used for welded joints and other applications where internal weld quality must be evaluated.
Potentially detectable defects include:
- Porosity.
- Slag inclusions.
- Certain lack-of-fusion conditions.
- Certain incomplete penetration defects.
- Other volumetric discontinuities.
Radiographic testing has specific limitations for planar defects, depending on their orientation relative to the radiation beam.
Radiation safety controls and qualified personnel are essential.
3.6 Magnetic Flux Leakage (MFL) and Electromagnetic Inspection
Magnetic flux leakage uses a magnetic field to examine ferromagnetic tubular products.
When material loss or certain discontinuities disturb the magnetic field, leakage flux can be detected by sensors.
MFL is commonly used for identifying metal-loss conditions in tubular inspection.
Electromagnetic inspection is a broader term covering several electromagnetic techniques, including MFL and eddy current methods.
The exact detection capability depends on the equipment, calibration and inspection procedure.
4. Hydrostatic Testing vs NDT: Main Differences
Hydrostatic testing and NDT should not be treated as interchangeable methods.
They provide different types of quality information.
| Comparison | Hydrostatic Testing | NDT |
|---|---|---|
| Main Purpose | Verify pressure integrity | Detect and evaluate selected discontinuities |
| Working Principle | Internal liquid pressure | Ultrasonic, electromagnetic, magnetic, optical or radiographic techniques |
| Test Medium | Water or specified liquid | Depends on the inspection method |
| Detects Leakage | Yes, under specified test conditions | Not generally a direct pressure leak test |
| Detects Internal Defects | Only when they affect pressure integrity or cause leakage | Certain internal defects can be detected |
| Wall Thickness Measurement | Not a direct measurement method | UT can measure wall thickness |
| Surface Defects | Only if they affect pressure integrity | MT and PT can detect suitable surface defects |
| Internal Cracks | Not reliably | UT and RT can detect certain defects |
| Pipe Damage | Test may impose pressure loading | Conventional NDT methods are designed to avoid damaging the component |
| Typical Application | Pressure-containing pipe products | Material and weld inspection |
It is important to understand that hydrostatic testing is itself a form of nondestructive pressure testing in the broad sense of testing without intentionally destroying the component.
However, in steel pipe manufacturing and inspection practice, hydrostatic testing is commonly discussed separately from conventional flaw-detection NDT methods such as UT, ET, MT and RT.
5. Comparison of Common Steel Pipe Inspection Methods
The following table summarizes the main applications of different inspection techniques.
| Testing Method | Main Detection Target | Typical Application |
|---|---|---|
| Hydrostatic Testing | Leakage and pressure integrity | Pressure-containing pipes |
| Ultrasonic Testing | Internal and selected surface-connected discontinuities | Seamless pipes and weld seams |
| Eddy Current Testing | Surface and near-surface discontinuities | Conductive tubular products |
| Magnetic Particle Testing | Surface and near-surface cracks | Ferromagnetic steel pipes |
| Liquid Penetrant Testing | Surface-breaking discontinuities | Pipe ends and accessible surfaces |
| Radiographic Testing | Internal weld discontinuities | Welded pipe joints |
| Magnetic Flux Leakage | Metal loss and selected discontinuities | Ferromagnetic tubular products |
The choice of method depends on the pipe material, manufacturing process, defect type, product dimensions, applicable standard and required inspection coverage.
6. Which Steel Pipe Standards Require Hydrostatic Testing and NDT?
Inspection requirements are not identical for every steel pipe product.
The applicable requirements depend on the product specification, grade, manufacturing route, dimensions, supplementary requirements and purchase order.
The following standards provide useful examples.
6.1 ASTM A106/A106M
ASTM A106 covers seamless carbon steel pipe for high-temperature service.
The specification includes a hydrostatic test requirement.
It also provides for a nondestructive electric test as an alternative under specified conditions and subject to the applicable requirements.
This distinction is important when reviewing the inspection documentation for ASTM A106 Grade A, Grade B and Grade C pipes.
Buyers should verify the applicable edition and the selected inspection route rather than assuming that every pipe must undergo both tests.
6.2 ASTM A53/A53M
ASTM A53 covers black and hot-dipped, zinc-coated, welded and seamless steel pipe.
Its hydrostatic test requirements address leakage through the pipe body or weld seam, as applicable.
The standard also includes specific provisions concerning test pressures and product configurations.
The inspection test pressure should not be interpreted as the allowable working pressure of the pipe.
6.3 API 5L
API 5L applies to line pipe used in pipeline transportation systems.
It includes requirements for hydrostatic testing and nondestructive inspection, with requirements depending on pipe type, grade, product specification level and other applicable conditions.
For welded line pipe, weld seam inspection is particularly important.
The specified NDT method, coverage and acceptance requirements must be checked against the applicable edition and product category.
6.4 ASTM A312/A312M
ASTM A312 covers seamless, welded and heavily cold-worked austenitic stainless steel pipe.
The specification includes hydrostatic testing and provisions for a nondestructive electric test as an alternative under specified conditions.
The selected inspection route must be consistent with the applicable specification and purchase requirements.
6.5 ISO 10893 Series
The ISO 10893 series covers nondestructive testing of steel tubes.
Relevant parts include:
- ISO 10893-1: Automated electromagnetic testing for verification of hydraulic leak-tightness.
- ISO 10893-2: Automated eddy current testing.
- ISO 10893-3: Automated magnetic flux leakage testing.
- ISO 10893-4: Liquid penetrant testing.
- ISO 10893-5: Magnetic particle testing.
- ISO 10893-6 and ISO 10893-7: Radiographic testing.
- ISO 10893-8, ISO 10893-9 and ISO 10893-10: Ultrasonic testing of different tubular products and defect types.
- ISO 10893-11: Automated ultrasonic testing of the weld seam of welded steel tubes.
The applicable part should be selected according to the product type and inspection objective.
7. Does Passing a Hydrostatic Test Mean a Steel Pipe Is Defect-Free?
No.
Passing a hydrostatic test demonstrates that the tested pipe met the specified pressure-test acceptance requirements under the test conditions.
It does not prove that every part of the pipe is free from material discontinuities.
For example, a pipe may pass a hydrostatic test while containing:
- A non-through-wall internal crack.
- A small inclusion.
- A lamination that does not cause leakage during testing.
- Localized wall thickness variations.
- Certain surface defects.
- Manufacturing discontinuities that do not compromise pressure integrity at the test pressure.
This is why additional inspection methods may be required.
For example, ultrasonic testing can help identify internal discontinuities, while magnetic particle testing can reveal suitable surface cracks in ferromagnetic materials.
The required combination of tests should be defined by the applicable product specification and inspection plan.
8. How to Choose the Right Inspection Method for Different Steel Pipes
Different steel pipe products have different manufacturing processes and service requirements.
8.1 Seamless Steel Pipes
Seamless pipes do not contain a longitudinal weld seam, but they may still contain manufacturing discontinuities.
Potential inspection methods include:
- Hydrostatic testing.
- Ultrasonic testing.
- Eddy current testing.
- Magnetic flux leakage.
- Dimensional inspection.
UT is particularly useful when internal discontinuities or wall thickness variations must be evaluated.
8.2 ERW Steel Pipes
Electric Resistance Welded (ERW) pipes contain a longitudinal weld seam.
Inspection should consider both the pipe body and weld seam.
Potential methods include:
- Automated ultrasonic weld seam testing.
- Eddy current testing.
- Hydrostatic testing.
- Visual and dimensional inspection.
The required inspection coverage depends on the applicable product specification.
8.3 LSAW and SSAW Steel Pipes
Longitudinal Submerged Arc Welded (LSAW) and Spiral Submerged Arc Welded (SSAW) pipes contain welded seams.
Ultrasonic testing and radiographic testing may be used to evaluate weld integrity, depending on the specification and inspection procedure.
Hydrostatic testing is used to verify pressure integrity where required.
Weld seam inspection and pressure testing provide different information and should be considered complementary when both are specified.
8.4 Stainless Steel Pipes
Stainless steel pipes may be inspected using hydrostatic testing, ultrasonic testing, eddy current testing and other suitable methods.
The choice depends on whether the objective is to verify pressure integrity, evaluate internal defects or detect surface discontinuities.
Magnetic particle testing is generally limited to suitable ferromagnetic stainless steel grades. It should not be assumed to be suitable for all austenitic stainless steels.
9. What Should Be Included in a Steel Pipe Inspection Plan?
A properly prepared Inspection and Test Plan (ITP) should clearly identify the required inspection stages and acceptance criteria.
Typical items include:
1. Material Verification
- Steel grade.
- Chemical composition.
- Heat number and traceability.
- Material Test Certificate.
2. Dimensional Inspection
- Outside diameter.
- Wall thickness.
- Length.
- Ovality.
- Straightness.
- End preparation.
3. Mechanical Testing
- Tensile testing.
- Yield strength.
- Elongation.
- Hardness.
- Impact testing, where applicable.
4. Nondestructive Testing
- Ultrasonic testing.
- Eddy current testing.
- Magnetic particle testing.
- Radiographic testing, where applicable.
5. Hydrostatic Testing
- Test pressure.
- Holding time.
- Pressure recording.
- Leakage acceptance.
- Test result documentation.
6. Final Inspection
- Visual inspection.
- Surface condition.
- Marking.
- End protection.
- Packaging.
- Inspection documentation.
Not every product requires every test listed above. The final ITP must follow the applicable standard and purchase order.
10. What Should Buyers Check in a Steel Pipe Inspection Report?
When purchasing steel pipes, buyers should review the inspection documentation rather than relying only on a general statement that the products have passed quality inspection.
Important records include:
Hydrostatic Test Report
Check:
- Pipe identification.
- Heat or batch number.
- Test pressure.
- Holding time.
- Test equipment identification.
- Calibration status, where required.
- Test result.
- Inspection date.
NDT Report
Check:
- Inspection method.
- Applicable procedure and standard.
- Pipe identification and traceability.
- Inspection coverage.
- Equipment and calibration details.
- Personnel qualification, where applicable.
- Recorded indications.
- Acceptance criteria.
- Final result.
Material Test Certificate
The MTC should provide the required material and test information, including chemical composition, mechanical properties and product traceability.
Where third-party inspection is specified, the relevant inspection release documents and reports should also be checked.
11. Common Mistakes When Comparing Hydrostatic Testing and NDT
Mistake 1: Assuming Hydrostatic Testing Can Replace All NDT
Hydrostatic testing does not provide comprehensive internal flaw detection.
Mistake 2: Assuming All NDT Methods Detect the Same Defects
UT, ET, MT, PT and RT have different physical principles and detection capabilities.
Mistake 3: Treating Hydrostatic Test Pressure as Working Pressure
Hydrostatic inspection pressure is specified for testing and should not automatically be used as the pipe’s allowable operating pressure.
Mistake 4: Ignoring Inspection Coverage
A test performed on a limited area is not equivalent to full-length or full-volume inspection.
Mistake 5: Ignoring Calibration and Personnel Qualification
Inspection results are only reliable when suitable procedures, equipment and qualified personnel are used.
Mistake 6: Relying Only on a Certificate Without Checking Traceability
Inspection reports must be traceable to the actual pipe, heat number or production batch as required.
12. Frequently Asked Questions
Is hydrostatic testing considered NDT?
Hydrostatic testing is a nondestructive pressure test in the broad sense because the pipe is not intentionally destroyed. However, it is commonly treated as a separate pressure-integrity test rather than a conventional flaw-detection NDT method.
What is the difference between hydrostatic testing and ultrasonic testing?
Hydrostatic testing evaluates whether a pipe can withstand a specified internal pressure without unacceptable leakage. Ultrasonic testing uses sound waves to detect selected material discontinuities and measure wall thickness.
Can ultrasonic testing replace hydrostatic testing?
Not automatically. A product specification may permit an alternative inspection route in certain circumstances, but this must be explicitly allowed by the applicable standard and purchase requirements.
Does every steel pipe require hydrostatic testing?
Not necessarily. Requirements depend on the product standard, pipe type, grade, manufacturing process and agreed inspection route. Some specifications permit a qualified alternative nondestructive electric test.
What is the most commonly used NDT method for seamless steel pipes?
Ultrasonic testing and electromagnetic inspection are commonly used, depending on the defect type and product requirements. The appropriate method should be selected based on the applicable specification.
Which NDT method is suitable for detecting surface cracks?
Magnetic particle testing is suitable for surface and near-surface cracks in ferromagnetic materials. Liquid penetrant testing can detect surface-breaking defects in both ferromagnetic and non-ferromagnetic materials.
Can hydrostatic testing detect internal cracks?
It may reveal a crack if that discontinuity creates leakage or pressure-boundary failure under the test conditions. It cannot reliably detect every internal crack.
What is the difference between UT and ET?
UT uses high-frequency sound waves, while ET uses electromagnetic induction. Their detection capabilities differ according to defect orientation, depth, material properties and inspection setup.
What is the purpose of third-party inspection?
Third-party inspection provides independent verification of agreed product specifications, manufacturing controls, testing procedures and inspection results.
What should be specified when ordering steel pipes?
Buyers should specify the applicable standard, grade, outside diameter, wall thickness, length, manufacturing process, inspection requirements, test coverage, acceptance criteria and documentation requirements.
13. Conclusion
Hydrostatic testing and nondestructive testing are two important but different approaches to steel pipe quality verification.
Hydrostatic testing evaluates pressure integrity by applying internal liquid pressure under specified conditions. NDT methods such as ultrasonic testing, eddy current testing, magnetic particle testing and radiographic testing identify selected material and weld discontinuities without destroying the product.
Neither method alone can establish every aspect of steel pipe quality.
For reliable inspection, manufacturers and buyers should select testing methods according to the pipe material, manufacturing process, applicable product specification and intended service conditions.
A well-defined inspection plan combining the required pressure testing, NDT, dimensional verification and material testing provides a more complete basis for evaluating product quality before delivery.
Looking for Steel Pipes Manufactured and Inspected to International Standards?
When sourcing seamless, ERW, LSAW or SSAW steel pipes, specify the required ASTM, API or ISO standard, material grade, dimensions, hydrostatic testing requirements, NDT method and inspection coverage.
Request a quotation together with the relevant Material Test Certificate, hydrostatic test report, NDT report and dimensional inspection records.