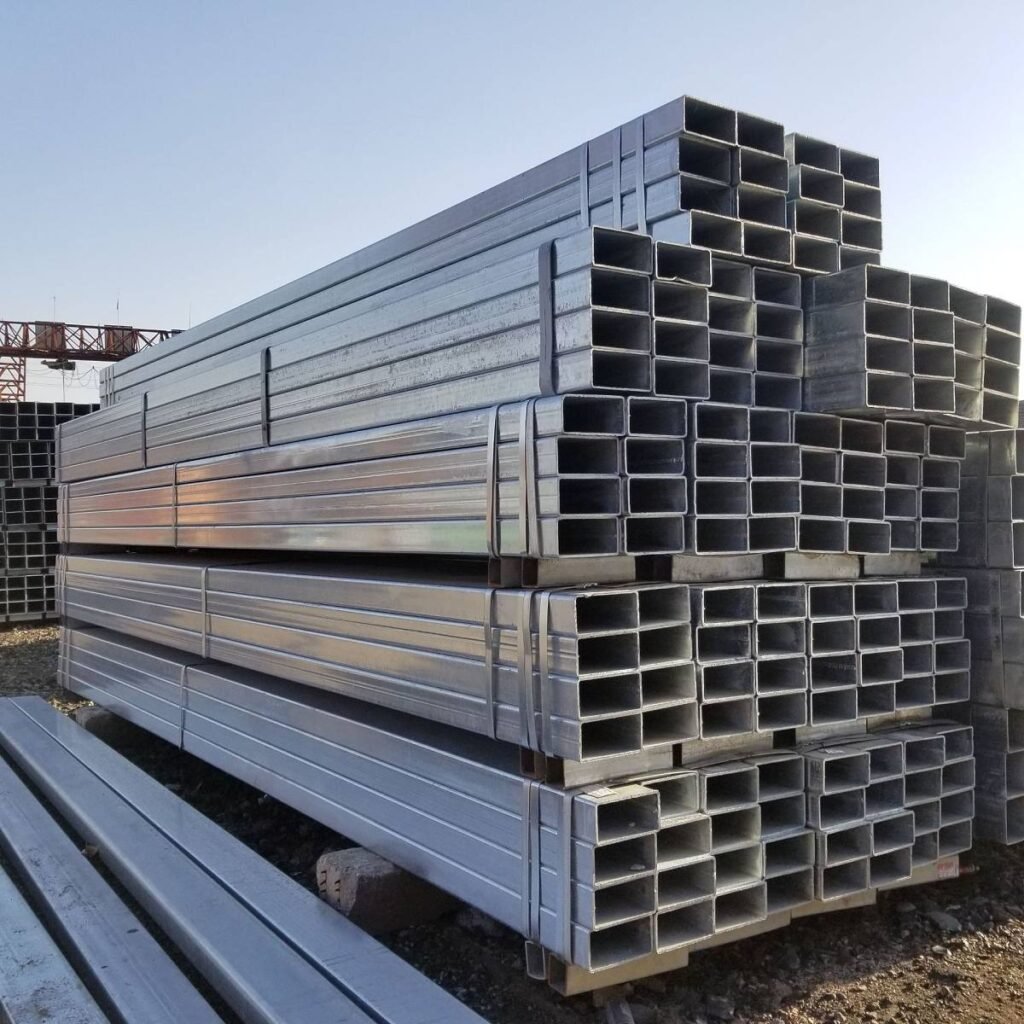
Two bundles of galvanized steel pipe can have the same diameter, wall thickness, and silver finish—and still offer very different corrosion protection.
The difference usually lies in how the zinc was applied, how much coating is present, and whether the inside of the pipe received the same protection as the outside. These details matter more than surface brightness, particularly when pipes will be exposed to rain, condensation, or difficult maintenance conditions.
For buyers comparing hot-dip galvanized and cold-galvanized steel pipe, the first step is to clarify the coating process.
What Does “Cold Galvanizing” Actually Mean?
“Cold galvanizing” is used inconsistently in the steel trade.
In some markets, it means electrogalvanizing, also called zinc electroplating. This process uses an electric current to deposit zinc onto the steel surface.
In English-language maintenance and coating products, “cold galvanizing” commonly means zinc-rich paint. The paint contains zinc particles in a binder and is applied by brush or spray.
These are different treatments. Neither should be accepted as an unspecified substitute for hot-dip galvanizing. The American Galvanizers Association specifically distinguishes zinc-rich paint from the metallurgically bonded coating formed by hot-dip galvanizing.
For a clear quotation, ask the supplier to use the exact term: hot-dip galvanized, electrogalvanized, or zinc-rich painted.
Hot-Dip Galvanizing vs. Electrogalvanizing at a Glance
| Feature | Hot-dip galvanized steel pipe | Electrogalvanized steel pipe |
|---|---|---|
| Process | Cleaned steel is immersed in molten zinc | Zinc is deposited using an electric current |
| Coating structure | Zinc-iron alloy layers form at the steel surface | A metallic zinc layer is electrodeposited |
| Coating thickness | Generally thicker | Generally thinner |
| Appearance | May be bright, spangled, or matte gray | Often smoother and more uniform |
| Corrosion protection | Commonly selected for prolonged outdoor exposure | Requires careful matching of thickness and finish to exposure |
| Internal coverage | Achievable with proper preparation and zinc flow | Must be specifically confirmed |
| Main buying consideration | Coating standard, thickness, coverage, and finish | Coating thickness, post-treatment, coverage, and service conditions |
Actual performance depends on the specified coating and operating environment. The process name alone is not a complete purchasing specification.
How Hot-Dip Galvanizing Protects Steel Pipe
During hot-dip galvanizing, properly cleaned steel is immersed in molten zinc, typically at around 450°C. Zinc reacts with the steel to form zinc-iron alloy layers, creating a metallurgical bond.
The coating protects the pipe in two ways. It separates the steel from the environment, and the zinc corrodes preferentially to provide sacrificial protection to nearby exposed steel. This protection has limits: large bare areas and significant installation damage still require repair.
For pipe buyers, the practical advantage is a robust metallic coating suited to handling and exposed service. However, proper cleaning and process control remain essential. A thick-looking surface does not excuse bare spots, blocked bores, or poor coverage.
Coating Thickness: Why It Matters
Under comparable exposure conditions, a thicker zinc coating generally provides a larger reserve against corrosion. This is a major reason hot-dip galvanizing is commonly selected for outdoor steelwork.
There is no universal thickness requirement for every galvanized pipe. The correct value depends on the applicable standard, product category, dimensions, and production process.
When comparing quotations, establish whether the requirement is expressed as:
- Coating thickness in micrometers.
- Coating mass in grams per square meter.
- Minimum local thickness.
- Average coating thickness or mass.
These terms are not interchangeable. A quotation stating an average value may not meet a specification requiring a minimum at individual inspection locations.
If coating mass is quoted, confirm how the surface area is defined. Figures for coated strip, finished pipe, and combined surfaces can follow different conventions.
Internal Protection: Check More Than the Outside
The outside of a pipe is easy to inspect. The inside often receives less attention until corrosion becomes a service problem.
Pipe galvanized after manufacture can receive internal and external protection when surfaces are properly cleaned and molten zinc can enter and drain freely. Tubular assemblies need suitable venting and drainage to achieve this.
For electrogalvanized pipe, do not assume the internal coating matches the exterior. Internal deposition depends on the plating arrangement and pipe geometry.
Where internal protection is required, put it in the purchase order. Ask how the supplier verifies coverage along the bore, including areas away from the pipe ends.
For fluid-carrying systems, coating coverage is only part of the decision. The conveyed medium, water chemistry, temperature, and applicable system requirements must also be considered. A coating suitable for outdoor atmospheric exposure is not automatically suitable for every internal service.
Pre-Galvanized Pipe Is Not the Same as Pipe Galvanized After Manufacture
This distinction explains many price differences.
Pre-galvanized tubing is made from steel strip that has already been zinc-coated. The strip is formed into a tube and welded. The original strip coating may have been applied by a continuous hot-dip process, so pre-galvanized does not automatically mean electrogalvanized.
Pipe galvanized after manufacture receives its coating after forming and welding.
The manufacturing sequence affects protection at the longitudinal weld seam and other worked areas. For pre-galvanized tubing, ask how both the external and internal weld seams are protected.
Batch hot-dip galvanizing and continuous coating processes have different scopes and specification requirements. They should not be treated as identical simply because both involve zinc.
When one offer is substantially cheaper, check the manufacturing route before negotiating the price.
Appearance: Brightness Does Not Prove Quality
A bright, smooth finish is attractive, but it does not establish coating thickness.
Hot-dip galvanized steel may have a shiny, spangled, or matte-gray appearance. Steel chemistry and processing can influence the finish without necessarily reducing coating performance.
Inspect for defects that affect use:
- Bare or damaged areas.
- Sharp zinc projections.
- Excessive deposits inside the bore.
- Coating interference at threads, grooves, or mating surfaces.
- Unacceptable repairs.
Use coating measurements and documented acceptance criteria to judge compliance. Photographs alone cannot confirm the coating process or thickness.
Which Coating Should You Choose?
Outdoor Pipework and Exposed Tubular Structures
Hot-dip galvanizing after manufacture is often a practical choice where pipes face repeated wetting, weather exposure, and limited access for maintenance.
Coastal, chemical, buried, and continuously immersed conditions need a more specific assessment. These environments may require an additional coating system or a different material.
Dry Indoor Applications
Electrogalvanizing may be suitable where exposure is mild and a controlled surface finish is important. Check for hidden moisture sources, including condensation, washdown, and leaks.
An indoor location does not always mean a dry environment.
Local Repairs and Maintenance
Zinc-rich paint can be useful for specified repairs to damaged galvanized coatings. It must be selected and applied according to the relevant repair requirements.
ASTM A780/A780M recognizes repair methods using zinc-based solder, zinc-rich paint, and sprayed zinc. Surface preparation and application requirements still apply; a product labeled “cold galvanizing spray” is not automatically compliant.
Price: Compare Equivalent Products
A lower galvanized pipe price may reflect a thinner coating, a different manufacturing route, different steel wall thickness, or reduced inspection requirements.
Compare offers on the same basis:
| Item | What to confirm |
|---|---|
| Base pipe | Standard, grade, diameter, wall thickness, and length |
| Coating process | Hot-dip after manufacture, pre-galvanized, or electrogalvanized |
| Coverage | External, internal, and weld-seam requirements |
| Coating acceptance | Applicable standard, thickness or mass, and sampling |
| End preparation | Plain, threaded, grooved, or other specified finish |
| Documentation | Pipe certification and coating inspection records |
| Packing | Protection against damage and trapped moisture |
For installed pipework, replacement cost includes dismantling, labor, access, and possible downtime. Those costs can outweigh the initial saving on a lighter coating.
What to Check When Galvanized Pipe Arrives
Match the bundle identification and certificates to the order. Verify dimensions, inspect accessible internal surfaces, and measure coating thickness using a suitable calibrated instrument and the agreed sampling procedure.
Also examine storage condition. White powdery staining can develop when wet galvanized pipes are tightly bundled without adequate airflow. Light staining does not necessarily mean serious coating loss, but heavy deposits require assessment.
Keep bundles clear of standing water and allow drainage and ventilation.
The right galvanized steel pipe is the one whose base material, coating, and manufacturing route match the job. Specify those details before ordering, and the difference between hot-dip and cold galvanizing becomes a measurable purchasing decision.