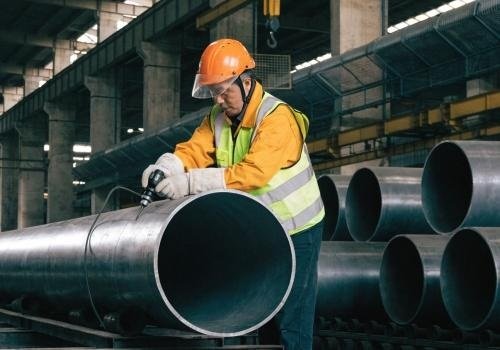
When seamless steel pipes arrive at a project site or warehouse, checking the quality before installation is an important step to avoid problems during fabrication and operation.
Although manufacturers normally provide inspection documents such as Mill Test Certificates (MTC), dimensional reports and test records, buyers should still perform basic incoming inspection after receiving the pipes.
Issues such as incorrect dimensions, surface defects, wrong material grade, transportation damage or missing traceability can create significant problems later.
A professional receiving inspection does not always require complex laboratory equipment. In many cases, the quality of seamless steel pipes can be quickly evaluated through four practical methods:
- Visual inspection
- Dimensional measurement
- Material and certificate verification
- Non-destructive testing confirmation
These methods help buyers identify obvious quality problems before the pipes enter production or installation.
Why Is Incoming Inspection Important for Seamless Steel Pipes?
Seamless steel pipes are widely used in demanding applications such as:
- Oil and gas pipelines
- Boilers
- Heat exchangers
- Petrochemical plants
- Pressure equipment
- Mechanical manufacturing
- Structural applications
Many of these applications involve high pressure, high temperature or corrosive environments. A pipe with incorrect material, excessive dimensional deviation or hidden defects may affect equipment safety and service life.
Quality inspection is therefore not only a manufacturing responsibility but also an important part of project quality control.
Common inspection methods for seamless steel pipes include dimensional inspection, surface examination, mechanical testing, hydrostatic testing and non-destructive testing such as ultrasonic or eddy current inspection.
Method 1: Check the Surface Quality Through Visual Inspection
The first and fastest inspection method is visual examination.
Before using measuring equipment, inspect the overall appearance of the seamless steel pipes.
What Should Be Checked?
Surface Cracks
Cracks are one of the most serious defects in steel pipes.
Possible causes include:
- Improper rolling process
- Excessive stress during manufacturing
- Cooling problems
- Transportation damage
A qualified seamless pipe should have a smooth surface without visible cracks.
Surface Pits and Corrosion
Check whether the pipe surface has:
- Rust spots
- Corrosion pits
- Deep scratches
- Surface peeling
Light surface oxidation may occur during storage and transportation, but serious corrosion can reduce the effective wall thickness.
For pipes intended for pressure applications, corrosion depth should be carefully evaluated.
Straightness
Place the pipe on a flat surface or inspect visually along its length.
Excessive bending may indicate:
- Improper handling
- Transportation damage
- Manufacturing problems
Straightness is particularly important for machining, welding and installation.
Pipe Ends
Inspect both ends carefully.
Check:
- Bevel condition
- End deformation
- Burrs
- Damage from loading and unloading
For pipes requiring welding, damaged bevels may affect welding quality.
Surface Inspection Limitations
Visual inspection is useful for identifying obvious defects, but it cannot detect internal defects.
Problems such as:
- Internal cracks
- Laminations
- Inclusions
- Hidden wall defects
require additional inspection methods.
Method 2: Measure Pipe Dimensions
The second quick method is dimensional inspection.
A seamless steel pipe must match the ordered specifications.
Important dimensions include:
- Outside diameter (OD)
- Wall thickness (WT)
- Length
- Straightness
- Ovality
- Pipe weight
Check Outside Diameter
Use:
- Vernier caliper
- Diameter tape
- Laser measuring equipment
Measure several locations along the pipe because diameter variation may occur.
Incorrect outside diameter may create problems during:
- Installation
- Welding
- Connection with fittings
- Equipment assembly
Check Wall Thickness
Wall thickness is one of the most important quality indicators.
Insufficient wall thickness may reduce:
- Pressure capacity
- Mechanical strength
- Service life
Portable ultrasonic thickness gauges are commonly used because they allow non-destructive thickness measurement. Ultrasonic thickness measurement determines wall thickness by analyzing the travel time of ultrasonic waves through the material.
For critical applications, buyers should compare actual measurements with:
- Purchase specification
- ASTM/API requirements
- Project tolerance requirements
Check Pipe Length
Incorrect pipe length may affect:
- Fabrication planning
- Material calculation
- Installation efficiency
Confirm whether the supplied pipes meet requirements for:
- Random length
- Double random length
- Fixed length
Check Weight
Pipe weight can also provide a quick indication of whether the supplied dimensions are close to the specification.
Significant weight differences may indicate:
- Incorrect wall thickness
- Incorrect diameter
- Wrong material size
For large quantities, weight verification is an efficient receiving inspection method.
Method 3: Verify Material Grade and Documentation
A seamless steel pipe may look correct externally but still have the wrong material.
This is one of the most important checks for industrial buyers.
A pipe marked as:
- ASTM A106 Grade B
- API 5L X52
- ASTM A335 P22
- ASTM A312 TP316
must actually meet the required chemical composition and mechanical properties.
Check the Mill Test Certificate (MTC)
The Mill Test Certificate usually contains:
- Manufacturer information
- Heat number
- Chemical composition
- Mechanical properties
- Heat treatment condition
- Test results
- Applicable standard
Important information includes:
Heat Number
The heat number connects the physical pipe with the original steel production record.
It provides traceability from:
Steel melting → Pipe manufacturing → Testing → Delivery
Chemical Composition
Check elements such as:
- Carbon (C)
- Manganese (Mn)
- Silicon (Si)
- Chromium (Cr)
- Nickel (Ni)
- Molybdenum (Mo)
Different grades require different chemical limits.
For example:
- ASTM A106 carbon steel pipe has different chemistry from ASTM A335 alloy pipe.
- 304 stainless steel differs from 316 stainless steel mainly because of alloy additions such as molybdenum.
Mechanical Properties
Review:
- Yield strength
- Tensile strength
- Elongation
These values confirm whether the pipe meets the required mechanical performance.
Use PMI Testing When Necessary
Positive Material Identification (PMI) is a fast method to verify alloy composition.
PMI is especially useful for:
- Stainless steel pipes
- Alloy steel pipes
- Cr-Mo pipes
- High-temperature applications
It can quickly identify whether the actual material matches the specified grade.
For example, PMI can help distinguish:
- 304 vs 316 stainless steel
- Carbon steel vs alloy steel
- Different Cr-Mo grades
This is particularly important in petrochemical and power plant projects where material mix-ups can cause serious failures.
Method 4: Confirm Non-Destructive Testing Results
The fourth method is reviewing or performing non-destructive testing (NDT).
NDT allows inspectors to identify defects without damaging the pipe.
Common methods include:
- Ultrasonic Testing (UT)
- Eddy Current Testing (ET)
- Magnetic Particle Testing (MT)
- Hydrostatic Testing
Ultrasonic Testing (UT)
Ultrasonic testing uses high-frequency sound waves to detect internal defects.
It can identify:
- Internal cracks
- Laminations
- Inclusions
- Wall thickness variations
UT is widely used for seamless steel pipe inspection because it can examine internal conditions without cutting the pipe.
Eddy Current Testing (ET)
Eddy current testing uses electromagnetic principles to detect surface and near-surface defects.
It is commonly used for:
- Thin-wall tubes
- Heat exchanger tubes
- Stainless steel tubes
Hydrostatic Testing
Hydrostatic testing checks whether the pipe can withstand specified pressure.
The pipe is filled with water and pressurized according to the applicable standard.
It helps identify:
- Leakage
- Pressure-related defects
- Weak areas
Hydrostatic testing is commonly required for pressure service applications.
Magnetic Particle Testing (MT)
Magnetic particle inspection is mainly used for ferromagnetic materials.
It can detect:
- Surface cracks
- Near-surface defects
It is often used together with other inspection methods.
Quick Comparison of the Four Inspection Methods
| Inspection Method | Detects | Suitable For |
|---|---|---|
| Visual Inspection | Surface damage, rust, cracks | All steel pipes |
| Dimensional Inspection | OD, WT, length deviation | All steel pipes |
| Material Verification | Wrong grade, chemistry issues | Alloy and critical pipes |
| NDT Inspection | Internal and surface defects | Pressure and critical applications |
Common Problems Found After Seamless Steel Pipe Delivery
Wrong Pipe Grade
The pipe appearance may be correct, but the material may not match the order.
Solution:
- Check MTC
- Perform PMI if necessary
Insufficient Wall Thickness
Possible causes:
- Manufacturing deviation
- Incorrect supply
- Measurement error
Solution:
- Perform ultrasonic thickness measurement
Surface Damage During Transportation
Possible problems:
- Dents
- Scratches
- Bent ends
- Rust
Solution:
- Inspect before unloading completely
- Record damage immediately
Missing Traceability
Without heat numbers and documentation, it becomes difficult to verify material quality.
Solution:
- Confirm markings before installation
What Should Buyers Check Before Accepting Seamless Steel Pipes?
A practical receiving checklist includes:
Appearance
✓ No visible cracks
✓ No severe corrosion
✓ No serious deformation
✓ Pipe ends acceptable
Dimensions
✓ Correct outside diameter
✓ Correct wall thickness
✓ Correct length
✓ Acceptable tolerance
Documentation
✓ Mill Test Certificate available
✓ Heat number matches marking
✓ Chemical composition meets requirements
✓ Mechanical properties meet requirements
Testing Records
✓ Hydrostatic test completed if required
✓ UT/ET records available if specified
✓ Inspection reports complete
How to Quickly Judge Seamless Steel Pipe Quality?
For most receiving inspections, the following sequence is efficient:
Step 1: Check Marking
Confirm:
- Manufacturer
- Grade
- Heat number
- Standard
Step 2: Inspect Appearance
Look for:
- Cracks
- Rust
- Damage
- Deformation
Step 3: Measure Dimensions
Check:
- Diameter
- Wall thickness
- Length
Step 4: Verify Documents and Testing
Confirm:
- MTC
- NDT reports
- Inspection certificates
This four-step process can quickly identify most common quality issues before the pipes enter production.
Conclusion
Checking seamless steel pipe quality after delivery does not always require complicated laboratory testing.
Through four practical methods:
- Visual inspection
- Dimensional measurement
- Material and certificate verification
- Non-destructive testing confirmation
buyers can quickly evaluate whether the supplied pipes match the purchase requirements.
For critical applications such as oil and gas pipelines, boilers, pressure equipment and petrochemical systems, incoming inspection should always be combined with complete documentation review and professional testing.
A reliable seamless steel pipe is not only defined by appearance. True quality comes from correct material, accurate dimensions, controlled manufacturing and complete traceability.