
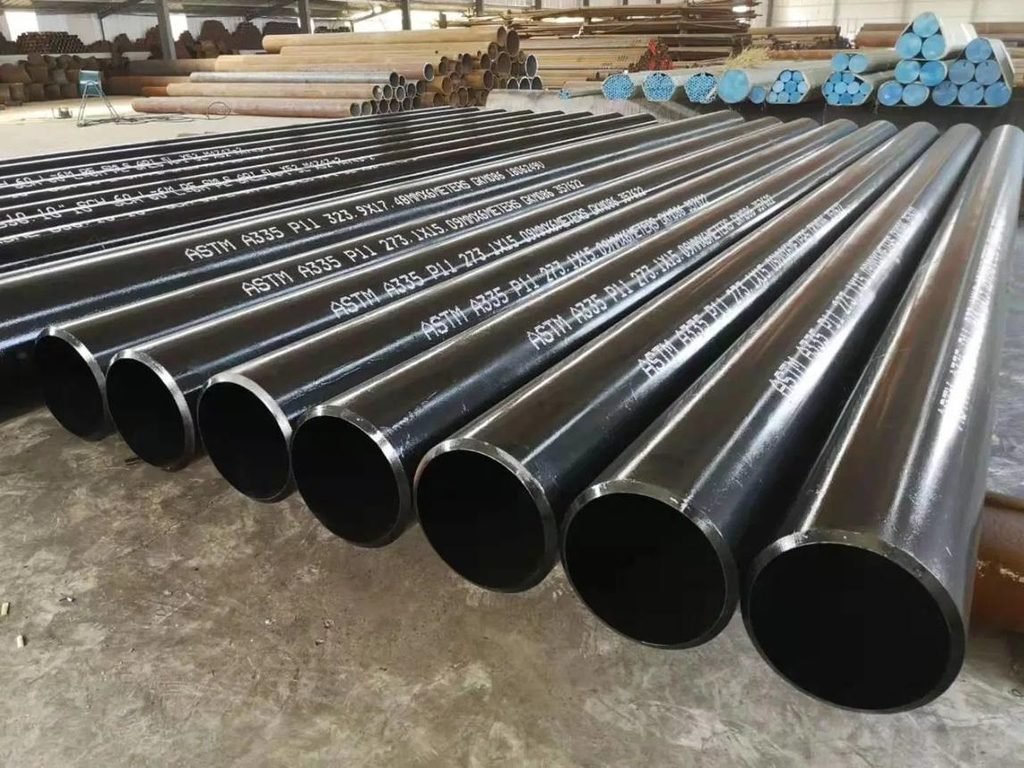
1. What Is Alloy Steel Heat Treatment?
Alloy steel heat treatment is a controlled thermal process used to modify the microstructure and mechanical properties of alloy steel. By controlling heating temperature, holding time, and cooling rate, manufacturers can adjust hardness, tensile strength, yield strength, toughness, ductility, and resistance to wear.
For alloy steel pipes, heat treatment is an important part of the manufacturing process. Hot forming, rolling, piercing, and other manufacturing operations can produce non-uniform microstructures and residual stresses. An appropriate heat treatment cycle helps establish the required metallurgical condition and mechanical properties.
The specific treatment depends on the chemical composition, pipe dimensions, wall thickness, manufacturing route, and applicable product specification.
Common heat treatment processes for alloy steel include:
- Annealing
- Normalizing
- Quenching
- Tempering
- Normalizing and tempering
- Quenching and tempering
- Stress relieving
These processes serve different purposes. They should not be treated as interchangeable options without considering the steel grade and required delivery condition.
2. Why Is Heat Treatment Important for Alloy Steel?
Alloy steel contains elements such as chromium, molybdenum, nickel, manganese, and vanadium. These elements influence hardenability, strength, toughness, high-temperature performance, and other material characteristics.
However, alloy composition alone does not determine the final mechanical properties. The thermal history of the steel also plays an important role.
Proper heat treatment can provide several benefits.
Improved mechanical strength
Quenching and tempering can develop a high-strength microstructure suitable for components exposed to mechanical loads and pressure.
Controlled hardness
Heat treatment allows manufacturers to adjust hardness according to the intended application and product specification.
Improved toughness
Tempering after hardening reduces the brittleness of the as-quenched structure and helps achieve a more suitable balance between strength and toughness.
Microstructural refinement
Normalizing can produce a more uniform microstructure and refine the grain structure in suitable steels.
Reduced residual stress
Stress-relief treatment can reduce residual stresses generated during welding, forming, machining, and other manufacturing operations.
For pressure-containing alloy steel pipes, the objective is not simply to achieve maximum hardness. The material must meet the specified combination of strength, toughness, ductility, and other service-related requirements.
3. Main Heat Treatment Processes for Alloy Steel
3.1 Annealing
Annealing involves heating steel to a specified temperature, holding it for a defined period, and cooling it under controlled conditions.
The purpose depends on the type of annealing process and the steel composition.
Common forms include:
- Full annealing
- Isothermal annealing
- Subcritical annealing
- Spheroidizing annealing
Main objectives:
- Reduce hardness
- Improve machinability
- Increase ductility
- Reduce certain residual stresses
- Obtain a more suitable microstructure for subsequent processing
Annealing is commonly used when alloy steel requires improved machinability or a softer condition before further manufacturing operations.
The temperature and cooling method must be selected according to the specific alloy composition and required microstructure.
3.2 Normalizing
Normalizing involves heating steel into the appropriate austenitizing temperature range, holding it until the required transformation occurs, and then cooling it in still or controlled air.
During heating, the steel develops an austenitic structure. During cooling, a new microstructure forms according to the steel composition and cooling conditions.
Main objectives:
- Refine grain structure
- Improve microstructural uniformity
- Reduce the effects of previous thermal or mechanical processing
- Establish a suitable starting condition for subsequent heat treatment
Normalizing is commonly applied to carbon steel and low-alloy steel products.
For alloy steel pipes, normalizing may be used as a final heat treatment or as part of a normalizing-and-tempering process, depending on the applicable specification.
3.3 Quenching
Quenching is a hardening process in which steel is heated to the required austenitizing temperature and then rapidly cooled using a suitable quenching medium.
Common quenching media include:
- Water
- Oil
- Polymer solutions
- Forced gas or air, where appropriate
For hardenable alloy steels, rapid cooling can transform austenite into martensite or other hardened transformation products, depending on the cooling rate and chemical composition.
Main objectives:
- Increase hardness
- Improve strength
- Develop a hardened microstructure
- Prepare the steel for subsequent tempering
Quenching must be carefully controlled. Excessive cooling severity or non-uniform cooling can result in cracking, distortion, and high residual stress.
For thick-wall alloy steel pipes, controlling the temperature difference between the outer surface and inner wall is particularly important.
3.4 Tempering
Tempering is generally performed after quenching. It involves reheating hardened steel to a temperature below its lower critical transformation temperature, holding it for a specified period, and then cooling it.
The tempering temperature has a direct influence on the final mechanical properties.
Main objectives:
- Reduce brittleness
- Relieve part of the residual stress
- Adjust hardness
- Improve toughness and ductility
- Stabilise the microstructure
In general, increasing the tempering temperature within the appropriate range reduces hardness and strength while improving toughness and ductility. The actual response depends on alloy composition and the tempering condition.
For high-strength alloy steel pipes, tempering is essential for achieving the mechanical properties required by the product specification.
3.5 Quenching and Tempering (Q&T)
Quenching and tempering is a combined heat treatment process widely used for alloy structural steels and certain alloy steel pipes.
The process consists of two main stages:
- Quenching: The steel is heated to the specified austenitizing temperature and rapidly cooled to produce a hardened microstructure.
- Tempering: The quenched steel is reheated to a specified temperature to adjust hardness, strength, toughness, and ductility.
The final microstructure in many quenched-and-tempered low-alloy steels is tempered martensite, although the exact structure depends on the steel grade and cooling conditions.
Q&T is used when a combination of high strength and adequate toughness is required.
Typical applications include:
- High-strength alloy steel pipes
- Oilfield tubular products
- Mechanical engineering components
- Pressure-containing equipment
- Heavy-duty structural components
3.6 Stress-Relief Heat Treatment
Stress-relief heat treatment involves heating steel below the relevant transformation temperature and holding it for a specified period before controlled cooling.
It is used to reduce residual stresses introduced by:
- Welding
- Cold forming
- Machining
- Hot forming
- Other manufacturing operations
Stress relief is particularly relevant to welded assemblies and fabricated pressure equipment.
It should not be confused with full annealing or quenching and tempering. These processes produce different metallurgical results.
4. Comparison of Alloy Steel Heat Treatment Processes
| Process | Main purpose | Typical cooling method | Main effect |
|---|---|---|---|
| Annealing | Soften steel and improve machinability | Furnace or controlled cooling | Lower hardness and improved ductility |
| Normalizing | Refine and homogenise structure | Air cooling | More uniform microstructure |
| Quenching | Develop a hardened structure | Water, oil or specified medium | Increased hardness and strength |
| Tempering | Adjust quenched properties | Air or specified cooling | Improved toughness and reduced brittleness |
| Quenching and Tempering | Balance strength and toughness | Quenching followed by tempering | High-strength, tempered structure |
| Stress Relieving | Reduce residual stress | Controlled cooling | Improved dimensional and stress stability |
The cooling method shown is general guidance. The actual cooling procedure must follow the relevant material specification and heat treatment procedure.
5. Heat Treatment Requirements for ASTM A335 Alloy Steel Pipes
ASTM A335 covers seamless ferritic alloy-steel pipe intended for high-temperature service.
Common grades include P5, P9, P11, P22, and P91. These grades contain different alloying elements and have different heat treatment requirements.
ASTM A335 P11
P11 is a chromium-molybdenum alloy steel commonly used in high-temperature applications.
Its heat treatment routes under the applicable specification include full or isothermal annealing, or normalizing and tempering.
P11 is commonly considered for boiler and high-temperature piping systems where elevated-temperature strength and oxidation resistance are required.
ASTM A335 P22
P22 is another chromium-molybdenum alloy steel, with a higher chromium and molybdenum content than P11.
It is used in power generation and other high-temperature service applications.
Its heat treatment requirements differ from those of P11 and must be checked against the applicable edition of ASTM A335.
ASTM A335 P91
P91 is a modified 9Cr-1Mo-V alloy steel developed for high-temperature applications requiring elevated creep strength.
Unlike many conventional low-alloy steel grades, P91 requires particularly careful control of normalizing and tempering or quenching and tempering.
For ASTM A335/A335M-24, the referenced heat treatment conditions include:
| Grade | Heat treatment route | Specified temperature range |
|---|---|---|
| P91 | Normalizing or austenitizing | 1040–1080°C |
| P91 | Tempering | 730–800°C |
These values are specific to the cited specification edition and should not be applied automatically to other grades or product forms.
P91 requires strict control of heat treatment temperature, holding time, cooling conditions, and subsequent inspection. Incorrect heat treatment can significantly affect its creep strength and microstructure.
Important: ASTM A335 is a product specification, not a universal heat treatment recipe. The applicable grade, manufacturing route, and current contractual specification determine the required treatment. Always verify the original standard before establishing production parameters.
6. How Is Alloy Steel Pipe Heat Treatment Performed?
In industrial pipe manufacturing, heat treatment is normally carried out using dedicated furnaces and controlled cooling equipment.
A typical quenching-and-tempering production route includes the following stages.
Step 1: Pipe preparation
Pipes are inspected and prepared for loading. Their grade, dimensions, wall thickness, and previous manufacturing condition are checked.
Step 2: Heating
The pipes enter a heat treatment furnace and are heated to the specified temperature.
Temperature uniformity is important because uneven heating can result in inconsistent microstructural transformation.
Step 3: Holding
The pipes remain at the specified temperature for the required period.
Holding time depends on material composition, wall thickness, pipe dimensions, and the approved heat treatment procedure.
Step 4: Quenching
After austenitizing, the pipes are transferred to the designated quenching system.
Depending on the material and process, cooling may use water, oil, polymer solution, or another specified medium.
For pipe products, internal and external cooling uniformity must be considered to avoid excessive thermal gradients.
Step 5: Tempering
The quenched pipes are reheated in a tempering furnace to obtain the specified mechanical properties.
Temperature and holding time must be controlled throughout the batch.
Step 6: Cooling and straightening
Following tempering, the pipes are cooled under controlled conditions. Straightening may be required to meet dimensional and straightness requirements.
Step 7: Inspection and testing
Finished pipes undergo the required mechanical, dimensional, and non-destructive examinations.
The final results are compared with the applicable product specification and purchase order.
7. Quality Control After Alloy Steel Heat Treatment
Heat treatment quality cannot be evaluated by furnace temperature records alone. The finished product must demonstrate that the specified properties have been achieved.
Important inspection and testing activities include the following.
Mechanical Property Testing
Tensile testing is used to determine:
- Yield strength
- Tensile strength
- Elongation
Impact testing may also be required to evaluate toughness at the specified test temperature.
Hardness Testing
Hardness testing is used to verify whether the material falls within the specified hardness range.
Depending on the product specification, testing may use Brinell, Rockwell, or another approved method.
Metallographic Examination
Metallographic examination is used to evaluate the microstructure after heat treatment.
It can help identify:
- Grain structure
- Tempered martensitic structure
- Non-uniform transformation
- Undesirable phases
- Other microstructural abnormalities
For P91 and similar creep-resistant steels, microstructural control is particularly important.
Non-Destructive Testing
Depending on the product specification and purchase requirements, non-destructive testing may include:
- Ultrasonic Testing (UT)
- Eddy Current Testing (ET)
- Magnetic Particle Testing (MT)
- Radiographic Testing (RT), where applicable
These methods are used to identify relevant surface or internal discontinuities.
Dimensional Inspection
After heat treatment, pipes may be checked for:
- Outside diameter
- Wall thickness
- Length
- Straightness
- Ovality
- Surface condition
Quenching can introduce dimensional changes, so dimensional inspection is an important part of final product quality control.
8. Common Heat Treatment Defects in Alloy Steel Pipes
Incorrect heating, cooling, or process control can result in defects that affect pipe performance.
| Common issue | Possible cause | Potential control measure |
|---|---|---|
| Quenching cracks | Excessive thermal stress or unsuitable quenching conditions | Optimise cooling severity and process uniformity |
| Distortion | Uneven heating or cooling | Improve temperature uniformity and pipe handling |
| Excessive hardness | Incorrect tempering condition | Verify tempering temperature and holding time |
| Low strength | Incorrect austenitizing or tempering conditions | Review the approved heat treatment cycle |
| Non-uniform microstructure | Uneven heating or insufficient holding | Improve furnace control and load arrangement |
| Excessive grain growth | Overheating or excessive holding time | Control austenitizing temperature and time |
| Residual stress | Non-uniform thermal transformation | Optimise cooling and subsequent stress control |
Defect analysis should consider the steel chemistry, pipe dimensions, manufacturing history, and heat treatment records. A single corrective measure cannot address every failure mechanism.
9. How to Select the Right Heat Treatment for Alloy Steel Pipes
Selecting a heat treatment process requires a clear understanding of the material and its intended service conditions.
The following information should be established before approving a heat treatment procedure:
Material grade
Identify the exact alloy steel grade, such as ASTM A335 P11, P22, or P91.
Pipe dimensions
Outside diameter and wall thickness influence heating uniformity, holding time, cooling rate, and the resulting microstructure.
Required mechanical properties
Specify the required yield strength, tensile strength, elongation, hardness, and impact properties.
Operating conditions
Consider service temperature, pressure, mechanical loading, and the intended operating environment.
Applicable product standard
Confirm the standard edition, grade-specific heat treatment requirements, inspection requirements, and delivery condition.
Manufacturing route
The appropriate treatment may differ depending on whether the pipe is hot-finished, cold-finished, welded, or processed through another manufacturing route.
For procurement, the heat treatment condition should be clearly stated in the technical specification and supported by the required inspection documentation.
10. Frequently Asked Questions About Alloy Steel Heat Treatment
What is the most common heat treatment for alloy steel?
Quenching and tempering is widely used for alloy structural steels that require a combination of high strength and toughness. However, annealing and normalizing are also common, depending on the grade and application.
What is the difference between annealing and normalizing?
Both processes involve heating and controlled cooling, but they use different cooling conditions and produce different microstructural results.
Annealing generally uses slower cooling, often furnace cooling, to reduce hardness and improve machinability. Normalizing generally uses air cooling to produce a more refined and uniform structure.
Why is tempering necessary after quenching?
Quenching can produce a hard but brittle microstructure with significant residual stress. Tempering adjusts hardness and strength while improving toughness and reducing brittleness.
Do all alloy steel pipes require quenching and tempering?
No. Heat treatment requirements depend on the material grade, manufacturing process, product specification, and required delivery condition. Some alloy steel pipes may be supplied in annealed, normalized, normalized-and-tempered, or other specified conditions.
What is the heat treatment temperature for ASTM A335 P91?
Under ASTM A335/A335M-24, P91 uses a normalizing or austenitizing temperature range of 1040–1080°C, followed by tempering at 730–800°C. The applicable standard edition and production requirements must always be checked before processing.
How does heat treatment affect alloy steel pipe quality?
Heat treatment influences microstructure, strength, hardness, toughness, ductility, and dimensional stability. An appropriate process helps the finished pipe meet its specified mechanical and metallurgical requirements.
11. Conclusion
Heat treatment is a critical manufacturing operation for alloy steel pipes, particularly those used in high-temperature, high-pressure, and mechanically demanding environments.
Annealing, normalizing, quenching, and tempering each serve different purposes. The correct process depends on the alloy composition, pipe dimensions, required mechanical properties, and applicable product standard.
For ASTM A335 grades such as P11, P22, and P91, grade-specific heat treatment requirements must be followed to ensure the finished pipes achieve the required performance.
When purchasing alloy steel pipes, buyers should verify the material grade, heat treatment condition, mechanical test results, inspection records, and material test certificate before accepting the products.
Need alloy steel pipes for your project?
Specify the required grade, dimensions, applicable standard, heat treatment condition, and operating requirements to identify the appropriate alloy steel pipe for your application.