
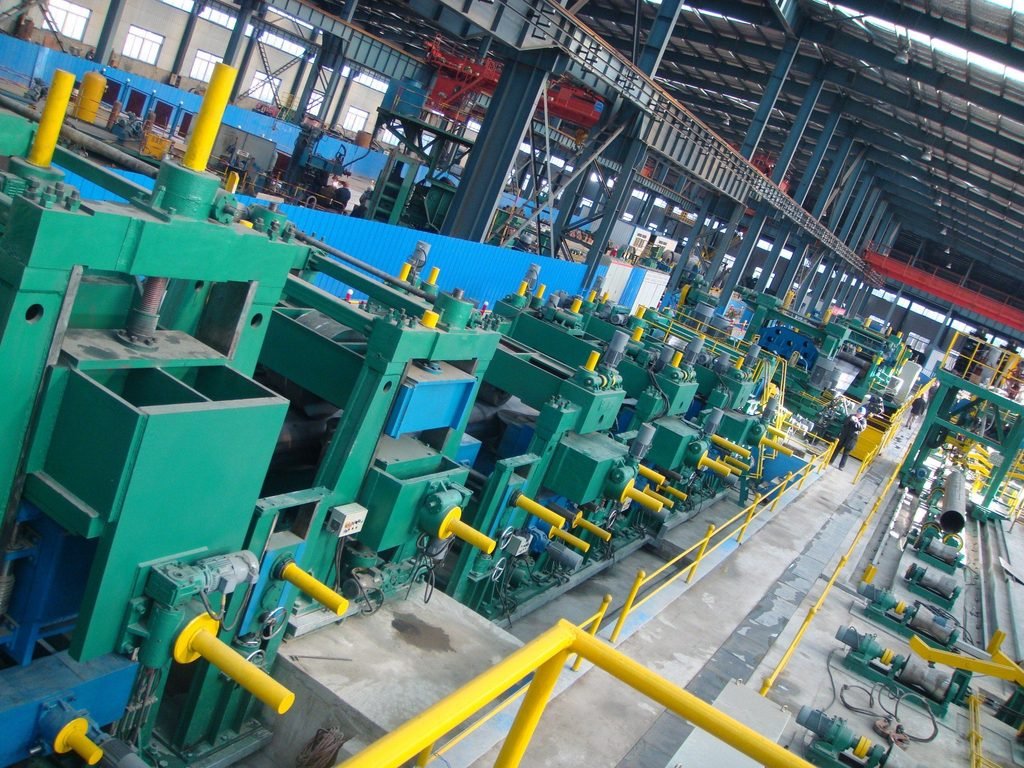
1. Introduction: Why Does the Manufacturing Process Matter for Steel Pipe Quality?
Steel pipes are used in a wide range of industrial applications, including oil and gas transportation, power generation, petrochemical processing, water supply, construction and mechanical engineering.
Although two steel pipes may have similar outside diameters, wall thicknesses and material grades, their manufacturing processes can be significantly different.
The manufacturing route influences how the steel is formed, how the pipe wall develops, whether a welded seam is present, and how heat treatment and subsequent processing affect the final product.
These factors can influence:
- Dimensional accuracy and wall thickness uniformity.
- Mechanical properties and microstructure.
- Weld seam integrity.
- Surface quality.
- Residual stress and hardness distribution.
- Resistance to defects during manufacturing.
- Suitability for specific operating conditions.
The main steel pipe manufacturing processes include seamless production, electric resistance welding (ERW), longitudinal submerged arc welding (LSAW) and spiral submerged arc welding (SSAW).
Each process has its own advantages, manufacturing limitations and quality control requirements.
Understanding these differences helps buyers select steel pipes according to their actual engineering requirements rather than simply comparing price or product dimensions.
2. Overview of the Main Steel Pipe Manufacturing Processes
Before comparing their effects on product quality, it is important to understand how the major manufacturing processes work.
2.1 Seamless Steel Pipe Manufacturing
Seamless steel pipes are manufactured without a longitudinal welded seam.
The production process generally begins with a solid steel billet, which is heated to a suitable temperature and pierced to create a hollow shell.
The shell is then elongated, rolled and sized to achieve the required outside diameter and wall thickness.
A typical seamless steel pipe manufacturing process includes:
- Steel billet preparation.
- Billet heating in a furnace.
- Rotary piercing.
- Mandrel rolling or another elongation process.
- Sizing or stretch-reducing.
- Cooling.
- Straightening.
- Heat treatment, where required.
- Cutting and end finishing.
- Nondestructive testing and final inspection.
The exact process sequence depends on the manufacturing equipment, pipe dimensions and material grade.
How does this process affect quality?
Because seamless pipes do not have a longitudinal weld seam, there is no weld metal or heat-affected zone along the pipe body.
However, seamless manufacturing does not mean that defects cannot occur.
Potential manufacturing issues include:
- Wall thickness eccentricity.
- Internal laps and seams.
- Surface cracks.
- Rolling marks.
- Geometric deviations.
- Localized variations in material properties.
Billet quality, heating temperature, piercing conditions and rolling parameters all influence the final product.
Seamless pipes are commonly used in high-temperature piping, mechanical engineering, boiler systems and selected high-pressure applications.
2.2 ERW Steel Pipe Manufacturing
Electric Resistance Welded (ERW) steel pipes are manufactured from steel strip or coil.
The steel strip passes through a series of forming rolls that gradually shape it into a cylindrical tube.
The two longitudinal edges are then heated by high-frequency electrical current and joined under pressure.
A typical ERW manufacturing process includes:
- Steel coil inspection.
- Coil uncoiling and leveling.
- Strip edge preparation.
- Roll forming.
- High-frequency resistance welding.
- Weld bead removal, where applicable.
- Weld seam heat treatment, where specified.
- Sizing and straightening.
- Cutting to length.
- Inspection and testing.
How does this process affect quality?
ERW manufacturing offers continuous production and efficient material utilization.
The process can produce pipes with consistent dimensions when strip quality, forming conditions and welding parameters are properly controlled.
However, weld seam quality is particularly important.
Potential defects include:
- Incomplete bonding.
- Lack of fusion.
- Oxide-related discontinuities.
- Weld seam cracks.
- Localized hardness variations.
- Misalignment of strip edges.
- Dimensional deviations.
Welding frequency, power input, squeeze pressure, line speed and edge preparation all influence weld quality.
For suitable products, online monitoring and heat treatment of the weld region help maintain consistent production quality.
ERW pipes are widely used in water transportation, structural applications, industrial piping and other applications covered by the relevant product specifications.
2.3 LSAW Steel Pipe Manufacturing
Longitudinal Submerged Arc Welded (LSAW) pipes are manufactured from steel plates.
The plate is formed into a cylindrical shape using a forming process such as UOE, JCOE or another qualified method.
The longitudinal seam is welded using submerged arc welding, commonly involving internal and external welding passes.
A typical LSAW manufacturing process includes:
- Steel plate inspection.
- Plate edge milling.
- Plate pre-bending.
- Pipe forming.
- Tack welding, where applicable.
- Internal submerged arc welding.
- External submerged arc welding.
- Mechanical expansion, where applicable.
- Nondestructive testing.
- Hydrostatic testing and final inspection.
How does this process affect quality?
LSAW manufacturing allows the production of large-diameter pipes using steel plate.
The plate can be inspected before forming, and the welding process can be controlled through qualified welding procedures.
However, welding introduces additional quality considerations.
Potential defects include:
- Lack of fusion.
- Incomplete penetration.
- Weld porosity.
- Slag inclusions.
- Cracks.
- Weld geometry deviations.
- Residual stresses.
Welding current, voltage, travel speed, heat input, consumable condition and plate edge preparation are important control variables.
Mechanical expansion, when used, can help improve dimensional consistency and reduce certain geometric variations.
LSAW pipes are commonly used in large-diameter oil and gas pipelines, water transmission systems and major infrastructure projects.
2.4 SSAW Steel Pipe Manufacturing
Spiral Submerged Arc Welded (SSAW) pipes are manufactured from steel strip or coil.
The strip is fed into a forming system at a controlled angle and gradually formed into a spiral cylindrical shape.
The spiral seam is then welded using submerged arc welding.
A typical SSAW manufacturing process includes:
- Steel coil inspection.
- Coil uncoiling and leveling.
- Strip edge preparation.
- Spiral forming.
- Internal submerged arc welding.
- External submerged arc welding.
- Cutting to the required length.
- Weld seam inspection.
- Hydrostatic testing, where required.
- Final dimensional inspection.
How does this process affect quality?
The spiral forming method allows manufacturers to produce large-diameter pipes using relatively narrow steel strip.
It also offers flexibility in adjusting pipe diameter through forming parameters and strip width.
However, the spiral weld seam is longer than a longitudinal seam in a pipe of comparable dimensions.
The quality of SSAW pipes depends on:
- Strip quality and dimensional consistency.
- Forming angle.
- Edge alignment.
- Welding parameters.
- Weld seam integrity.
- Pipe geometry.
- Nondestructive inspection coverage.
Potential defects include weld porosity, slag inclusions, lack of fusion, cracks and dimensional irregularities.
SSAW pipes are widely used in water transportation, municipal infrastructure, piling and selected pipeline applications.
3. How Do Manufacturing Processes Affect Steel Pipe Quality?
Different manufacturing processes influence different aspects of product quality.
The following sections explain the most important factors.
3.1 Dimensional Accuracy and Wall Thickness Uniformity
Dimensional accuracy is essential for pipe installation, connection, welding and pressure design.
The manufacturing process determines how the pipe is formed and how its dimensions are controlled.
Seamless Pipes
Wall thickness uniformity depends on billet quality, piercing alignment, rolling conditions and sizing control.
Eccentricity may occur when the hollow shell is not formed or rolled uniformly.
ERW Pipes
Outside diameter and wall thickness are strongly influenced by the incoming strip dimensions, forming rolls and sizing equipment.
The quality of the strip edges and forming alignment also affects the weld seam position.
LSAW Pipes
Plate thickness and forming accuracy are important factors.
Plate edge preparation, forming geometry and mechanical expansion influence the final pipe dimensions.
SSAW Pipes
Strip thickness, strip width, forming angle and forming tension influence the final diameter and geometry.
The spiral forming process also requires consistent alignment to maintain stable weld seam positioning.
Regardless of manufacturing method, dimensional inspection should verify:
- Outside diameter.
- Wall thickness.
- Length.
- Ovality.
- Straightness.
- End preparation.
The acceptance limits must follow the applicable product standard and purchase specification.
3.2 Mechanical Properties and Microstructure
Steel pipe mechanical properties are affected by steelmaking, forming temperature, deformation, cooling rate and heat treatment.
Important properties include:
- Yield strength.
- Tensile strength.
- Elongation.
- Hardness.
- Impact toughness.
- Ductility.
For seamless pipes, hot working and subsequent heat treatment influence the microstructure and mechanical properties throughout the pipe wall.
For ERW pipes, the welding thermal cycle creates a localized weld region and heat-affected zone (HAZ).
If the welding process and subsequent heat treatment are not properly controlled, the weld region may develop an undesirable microstructure or hardness distribution.
For LSAW and SSAW pipes, submerged arc welding introduces thermal cycles that affect the weld metal and HAZ.
The number of welding passes, heat input, cooling conditions and consumable selection can influence the final weld properties.
Heat treatment, when required, may be used to achieve the specified mechanical properties and improve the condition of particular regions.
It is important to remember that manufacturing method alone does not determine the final mechanical performance. The steel grade, product specification, heat treatment and inspection results must also be considered.
3.3 Weld Seam Quality
Weld seam quality is a major consideration for welded steel pipes.
Unlike seamless pipes, ERW, LSAW and SSAW pipes contain a longitudinal or spiral welded seam.
The manufacturing process determines the welding method and the associated quality control requirements.
| Manufacturing Method | Welding Process | Main Quality Control Focus |
|---|---|---|
| Seamless | No longitudinal weld | Billet quality, piercing and rolling defects |
| ERW | High-frequency resistance welding | Edge preparation, bonding and weld heat treatment |
| LSAW | Longitudinal submerged arc welding | Weld penetration, fusion and weld metal quality |
| SSAW | Spiral submerged arc welding | Spiral seam integrity, alignment and welding consistency |
A welded pipe should not automatically be considered inferior to a seamless pipe.
A properly manufactured and inspected welded pipe can meet demanding product specifications and service requirements.
The key is whether the welding process is qualified and whether the finished product satisfies the applicable acceptance criteria.
3.4 Surface Quality and Manufacturing Defects
Surface quality affects corrosion protection, coating adhesion, installation and overall product appearance.
Common manufacturing defects include:
- Scratches.
- Scale.
- Surface cracks.
- Laminations.
- Laps.
- Pitting.
- Weld undercut.
- Localized grinding marks.
For seamless pipes, surface conditions may be influenced by billet quality, heating and rolling.
For welded pipes, surface defects can arise during strip handling, forming, welding and subsequent processing.
Proper surface inspection, defect removal procedures and dimensional verification are essential.
Any repair or grinding operation must maintain the minimum required wall thickness and comply with the applicable product specification.
3.5 Residual Stress and Pipe Deformation
Residual stresses can develop during forming, welding, cooling and straightening.
In seamless pipes, uneven deformation and cooling may contribute to residual stress and geometric deviations.
In ERW pipes, localized welding heat and forming operations can influence the residual stress distribution.
In LSAW and SSAW pipes, plate or strip forming and welding introduce additional stress-related considerations.
Residual stresses may influence dimensional stability, fatigue behavior and susceptibility to certain environmentally assisted cracking mechanisms.
Mechanical expansion and appropriate heat treatment may be used where required by the manufacturing procedure and product specification.
4. Comparison of Four Main Steel Pipe Manufacturing Processes
The following table provides a practical comparison for steel pipe buyers.
| Comparison | Seamless | ERW | LSAW | SSAW |
|---|---|---|---|---|
| Starting Material | Solid billet | Steel strip or coil | Steel plate | Steel strip or coil |
| Manufacturing Method | Piercing and rolling | Roll forming and resistance welding | Plate forming and SAW | Spiral forming and SAW |
| Longitudinal Weld | None | Yes | Yes | Spiral weld |
| Typical Product Range | Small to large diameters, depending on mill capability | Commonly small to medium diameters | Commonly medium to large diameters | Commonly medium to large diameters |
| Main Quality Focus | Wall thickness, piercing and rolling quality | Weld bonding and dimensional control | Weld integrity and plate forming | Spiral seam quality and forming accuracy |
| Typical Inspection | UT, ET, dimensional and pressure testing as applicable | Weld inspection, UT/ET and pressure testing as applicable | Weld UT/RT and pressure testing as applicable | Weld UT/RT and pressure testing as applicable |
| Typical Applications | Pressure piping, boilers, mechanical tubes | Fluid transportation and structural uses | Large-diameter pipelines and infrastructure | Water transmission and infrastructure |
The actual diameter and wall thickness ranges depend on the manufacturer’s equipment and applicable product standard.
5. Which Manufacturing Process Produces the Best Quality Steel Pipe?
There is no single manufacturing process that produces the best steel pipe for every application.
The correct choice depends on the required material grade, dimensions, operating pressure, temperature, service environment, applicable standard and project specifications.
When Should Buyers Choose Seamless Steel Pipes?
Seamless pipes are suitable when:
- A product specification requires seamless manufacturing.
- A longitudinal weld seam is not desired.
- The required dimensions are within the manufacturer’s seamless production capability.
- The application involves specified high-temperature or pressure service.
Typical applications include boiler systems, mechanical engineering and selected oil and gas applications.
When Should Buyers Choose ERW Steel Pipes?
ERW pipes are suitable when:
- The required dimensions are available from qualified ERW production.
- High production efficiency is important.
- Consistent dimensional control is required.
- The pipe is intended for an application covered by the relevant ERW product specification.
Typical applications include structural tubes, water transportation and industrial piping.
When Should Buyers Choose LSAW Steel Pipes?
LSAW pipes are suitable when:
- Large-diameter welded pipes are required.
- Steel plate is the preferred starting material.
- The project specifies particular plate and weld inspection requirements.
- The product must meet applicable pipeline or pressure service specifications.
Typical applications include long-distance pipelines, oil and gas transportation and large infrastructure projects.
When Should Buyers Choose SSAW Steel Pipes?
SSAW pipes are suitable when:
- Large-diameter pipes are required.
- Spiral welded construction is permitted by the project specification.
- The application involves water transportation, piling or infrastructure.
- The manufacturer can demonstrate the required weld inspection and dimensional quality.
The buyer should verify that the spiral welded product is permitted by the applicable design code and project specification.
6. How Does Heat Treatment Affect Steel Pipe Quality?
Heat treatment is an important secondary manufacturing process for many steel pipe products.
It changes the microstructure and can influence strength, hardness, toughness and residual stress.
Common heat treatment processes include:
6.1 Normalizing
Normalizing involves heating steel to an appropriate temperature above its transformation range, followed by cooling in still air under controlled conditions.
It is commonly used to refine the microstructure and improve consistency in suitable steel grades.
6.2 Annealing
Annealing involves heating and controlled cooling to obtain a required metallurgical condition.
Depending on the steel grade and annealing procedure, it can improve ductility, reduce hardness and facilitate subsequent processing.
6.3 Quenching and Tempering
Quenching involves heating the steel to an appropriate austenitizing temperature and rapidly cooling it.
Tempering is then performed to obtain the required balance of strength, toughness and hardness.
This treatment is commonly used for selected alloy steel and high-strength pipe products.
6.4 Weld Seam Heat Treatment
For certain welded pipes, localized heat treatment may be used to control the metallurgical condition of the weld region.
For ERW/HFW pipes, weld seam heat treatment may be required to achieve the specified weld properties.
The actual treatment requirements depend on the product standard, grade and manufacturing procedure.
7. What Quality Inspection Is Required for Different Manufacturing Processes?
Inspection requirements should be selected according to the product standard, manufacturing process and intended application.
Common quality control activities include:
7.1 Chemical Composition Analysis
Chemical analysis verifies that the steel meets the specified material grade.
Important elements may include:
- Carbon.
- Manganese.
- Silicon.
- Sulfur.
- Phosphorus.
- Chromium.
- Nickel.
- Molybdenum.
- Vanadium.
The required elements and acceptance limits depend on the product specification.
7.2 Mechanical Testing
Mechanical tests may include:
- Tensile testing.
- Yield strength testing.
- Elongation testing.
- Hardness testing.
- Charpy impact testing.
- Flattening testing.
- Guided bend testing.
For welded pipes, certain tests may specifically evaluate the weld region.
7.3 Nondestructive Testing (NDT)
NDT is used to identify selected defects without destroying the product.
Common techniques include:
Ultrasonic Testing (UT): Uses sound waves to detect internal discontinuities and assess wall thickness.
Eddy Current Testing (ET): Uses electromagnetic induction to identify selected surface and near-surface discontinuities.
Radiographic Testing (RT): Uses X-rays or gamma rays to evaluate selected internal discontinuities, particularly in welds.
Magnetic Particle Testing (MT): Detects suitable surface and near-surface defects in ferromagnetic materials.
The required inspection coverage and acceptance criteria should be stated in the applicable specification.
7.4 Hydrostatic Testing
Hydrostatic testing verifies pressure integrity under specified test conditions.
The pipe is filled with liquid and pressurized to the required test pressure.
The test is used to identify leakage or pressure-boundary failure under the specified conditions.
It should not be considered a replacement for all NDT methods because it cannot reliably identify every internal or surface discontinuity.
7.5 Dimensional Inspection
Dimensional inspection verifies whether the finished pipe meets the required geometry.
Typical inspection items include:
- Outside diameter.
- Wall thickness.
- Length.
- Ovality.
- Straightness.
- End preparation.
- Bevel geometry.
8. Relevant Standards for Steel Pipe Manufacturing and Quality
International standards define manufacturing requirements, material properties, testing methods and acceptance criteria.
Common standards include:
| Standard | Main Application |
|---|---|
| API 5L | Steel line pipe for pipeline transportation systems |
| ASTM A106/A106M | Seamless carbon steel pipe for high-temperature service |
| ASTM A53/A53M | Welded and seamless carbon steel pipe |
| ASTM A335/A335M | Seamless alloy steel pipe for high-temperature service |
| ASTM A312/A312M | Austenitic stainless steel pipe |
| ASTM A333/A333M | Steel pipe for low-temperature service |
| ISO 3183 | Steel pipe for pipeline transportation systems |
| EN 10216 | Seamless steel tubes for pressure purposes |
| EN 10217 | Welded steel tubes for pressure purposes |
These standards do not all cover the same manufacturing processes.
For example, ASTM A106 is a seamless pipe specification, while API 5L covers several line pipe manufacturing routes subject to its requirements.
Buyers should confirm the applicable edition, product type, grade and supplementary requirements before placing an order.
9. Common Manufacturing Defects and Their Prevention
Different production processes introduce different manufacturing risks.
| Manufacturing Process | Potential Defects | Main Prevention Measures |
|---|---|---|
| Seamless | Wall thickness eccentricity, internal laps, surface cracks | Billet inspection, piercing alignment, rolling control |
| ERW | Incomplete bonding, weld cracks, hardness variation | Edge preparation, welding parameter control, seam heat treatment where required |
| LSAW | Lack of fusion, porosity, slag inclusions | Qualified welding procedures, consumable control, NDT |
| SSAW | Spiral seam defects, misalignment, dimensional deviation | Forming control, edge alignment, welding parameter monitoring |
A quality defect should be evaluated according to its location, size, orientation and the applicable acceptance criteria.
Not every indication represents an unacceptable defect. The final disposition should follow the governing standard and approved inspection procedure.
10. How to Evaluate a Steel Pipe Manufacturer’s Production Quality
When choosing a steel pipe manufacturer, buyers should evaluate more than the production equipment.
A reliable supplier should be able to demonstrate effective control over the entire manufacturing process.
Important evaluation points include:
1. Raw Material Control
Check whether the manufacturer verifies billet, plate or coil quality before production.
2. Manufacturing Process Control
Review forming parameters, welding procedures, heat treatment and dimensional control.
3. Quality Management System
Confirm whether the manufacturing facility operates an appropriate quality management system.
4. Inspection and Testing Capability
Check the availability of chemical analysis, mechanical testing, NDT and hydrostatic testing facilities.
5. Product Traceability
Verify whether heat numbers and production records can be traced through manufacturing and final delivery.
6. Nonconformance Management
Review how defective products are identified, repaired, retested and released.
7. Documentation
Request relevant MTCs, inspection reports, NDT records and dimensional inspection documents.
For project-based procurement, buyers may also require an Inspection and Test Plan (ITP), manufacturing procedure documentation and third-party inspection.
11. Frequently Asked Questions
Does seamless steel pipe always have better quality than welded steel pipe?
No. Seamless pipes have no longitudinal weld seam, but they can still contain manufacturing defects such as wall thickness eccentricity, internal laps and surface cracks.
Properly manufactured and inspected welded pipes can meet demanding technical specifications.
What is the difference between ERW and LSAW steel pipes?
ERW pipes are manufactured from steel strip or coil using high-frequency resistance welding. LSAW pipes are manufactured from steel plate using longitudinal submerged arc welding.
They differ in starting material, forming process, welding method and typical product dimensions.
Which manufacturing process is suitable for large-diameter steel pipes?
LSAW and SSAW are commonly used for large-diameter pipes. The choice depends on the required dimensions, wall thickness, project specification and manufacturing capability.
Does the manufacturing process affect wall thickness uniformity?
Yes. Seamless pipe wall thickness is influenced by piercing and rolling alignment. Welded pipe dimensions depend on strip or plate thickness, forming conditions, sizing and dimensional control.
Why is heat treatment important in steel pipe manufacturing?
Heat treatment controls the microstructure and can improve the required mechanical properties, including strength, hardness, ductility and toughness.
Can welded steel pipes be used in high-pressure applications?
Yes, provided the pipe is manufactured, tested and accepted in accordance with the applicable product specification and design requirements.
The manufacturing method alone does not determine whether a pipe is suitable for a particular pressure application.
What is the main quality difference between LSAW and SSAW pipes?
The main differences involve starting material, forming geometry and weld seam configuration.
LSAW pipes have a longitudinal weld, while SSAW pipes have a spiral weld. Their quality should be evaluated through the applicable dimensional, mechanical and weld inspection requirements.
Which inspection methods are commonly used for seamless pipes?
Depending on the specification, inspection may include ultrasonic testing, electromagnetic testing, dimensional inspection, mechanical testing and hydrostatic testing.
Which inspection methods are important for welded steel pipes?
Welded pipes may require weld seam UT, RT or other specified NDT methods, together with dimensional, mechanical and pressure testing as applicable.
What should buyers check before purchasing steel pipes?
Buyers should verify the product standard, manufacturing process, material grade, outside diameter, wall thickness, length, tolerances, inspection requirements, certifications and intended application.
12. Conclusion
Steel pipe manufacturing processes have a direct influence on product quality.
Seamless manufacturing eliminates the longitudinal weld seam but requires strict control of billet quality, piercing and rolling conditions.
ERW manufacturing offers efficient production and dimensional consistency when strip preparation and high-frequency welding are properly controlled.
LSAW manufacturing is suitable for many large-diameter applications, with weld integrity and plate forming accuracy being important quality considerations.
SSAW manufacturing provides flexibility in large-diameter pipe production, while requiring careful control of spiral forming, welding and dimensional accuracy.
There is no universally superior manufacturing method. The right choice depends on the material grade, pipe dimensions, operating conditions, product specification and inspection requirements.
For steel pipe buyers, understanding the relationship between manufacturing processes and product quality makes it easier to select suitable products, evaluate manufacturers and reduce technical risks during procurement.
Looking for a Steel Pipe Manufacturer for Your Project?
Whether your project requires seamless, ERW, LSAW or SSAW steel pipes, confirm the applicable standard, material grade, dimensions, manufacturing process and inspection requirements before placing an order.
Request a quotation with the relevant material certificates, inspection reports and technical specifications to ensure that the supplied products meet your project requirements.